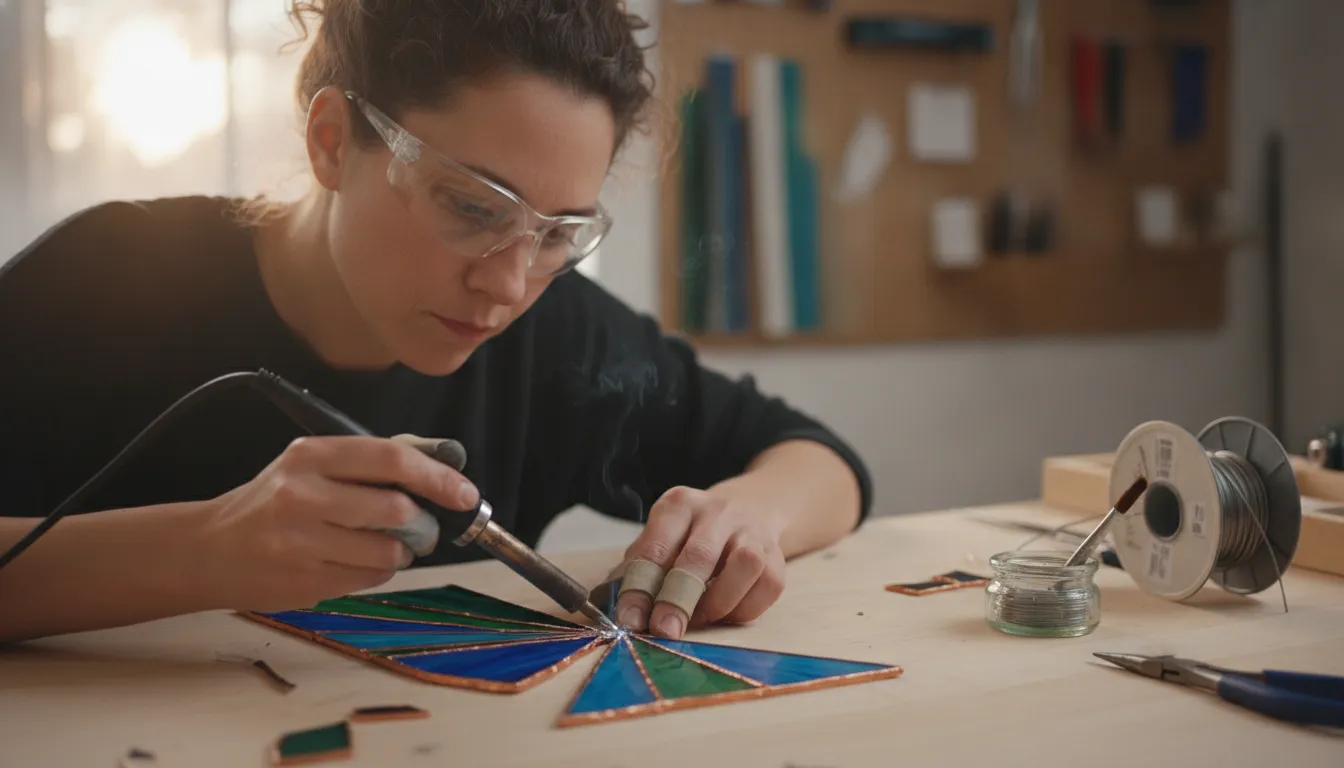
A clean stained glass seam is controlled by more than a hot iron. The result depends on a stable work surface, the right amount of flux, steady movement, and enough heat to join the materials without stressing the glass.
Shop stained glass tools and soldering supplies
Good stained glass soldering starts with a properly tinned, clean tip and a well-supported project. Copper foil seams need an even solder bead over the foil, while lead came joints require heat and solder applied carefully at the meeting point of the came. In both methods, ventilation, eye protection, hand hygiene, and a noncombustible work surface are essential. Small changes in heat, speed, and flux can turn a weak or lumpy seam into a smooth, durable joint.
Set up the tools and workspace before choosing an alloy or practicing a bead. This creates the control needed for copper foil and lead came techniques.
What You Need for a Safe, Controlled Soldering Session
A reliable stained glass soldering setup starts with control over the iron, work surface, fumes, and surrounding materials. Gather a temperature-controlled iron, stable stand, solder, flux, tip-cleaning material, tweezers or pliers, and a noncombustible work board. If you are comparing iron styles or features, see this stained glass soldering iron guide before choosing equipment.
Place the project on a fire-resistant, noncombustible surface that will not shift. Keep the iron in its stand when not in use, and never try to catch a falling iron. Keep cords, sleeves, and loose tools away from hot tips, molten solder, joints, and dross. Use tweezers, pliers, or clamps instead of placing fingers near the heat.
Ventilation is part of the setup. Work in a well-ventilated area with local exhaust, such as a benchtop extractor that draws smoke away from your breathing zone. Recirculating filtration is not considered acceptable for lead-containing solder. Wear eye protection, keep food and drink away, and review the safety data sheets for your solder and flux. When practical, choose rosin-free or lead-free materials appropriate for the project.
Lead-containing solder requires disciplined hygiene. Keep hands away from your face, then wash them with soap and water after the session. Damp-wipe the work surface instead of using compressed air or dry wipes. Collect solder scraps and dross in a lidded container for appropriate disposal. Switch off and unplug the iron, let it cool completely, and allow the panel to cool before lifting, turning, or inspecting it.
How to Choose Solder, Flux, and Heat for the Seam
Your materials should match the seam you are trying to build. For many copper-foil projects, 60/40 solder is a practical starting point because it melts and flows readily, making it easier to form a consistent bead. 50/50 solder is useful when you want a firmer, more controlled line, but it can feel less forgiving while you are learning to keep the bead smooth.
Pay attention to wire diameter as well as alloy. Solder is commonly sold by diameter rather than a universal wire gauge, so check the spool label. A 1/8-inch (3 mm) 60/40 wire is a practical size for building a continuous bead. A thinner wire can make small tack points and repairs easier to meter, while a thicker wire adds solder faster. Choose the diameter that matches the seam and your pace instead of feeding more solder than the joint can accept.
Choosing a solder alloy for stained glass soldering
| Alloy | Flow and handling | Useful application |
|---|---|---|
| 60/40 | Flows readily and is generally easier to move into a smooth bead. | A versatile choice for copper-foil seams and general practice. |
| 50/50 | Can feel more controlled, but may require closer attention to movement and heat. | Useful when a project or technique calls for a firmer alloy, provided you can maintain an even seam. |
Flux helps solder wet and bond to the copper foil or other metal. Apply a light, even coating to the seam rather than flooding it. Too little flux can leave irregular coverage or exposed foil. Too much may spatter and contribute to pits or bubbles. For a more detailed process, see how to apply flux to copper foil.
Which flux type should you use?
Liquid, gel, and paste fluxes can all be useful for stained glass soldering. Liquid flux spreads quickly across a long copper foil seam, gel stays where you brush it, and paste offers a thicker film for a small joint or a vertical area. Choose a flux labeled for stained glass and follow its product instructions. The container format changes how much control you have, not the need for a clean metal surface, a thin application, ventilation, and prompt residue removal.
Avoid substituting plumbing flux or an unverified acid product. If solder beads up, stop rather than adding more flux repeatedly. Clean the joint, inspect for oxidation or contamination, apply a small amount of the chosen stained glass flux, and test the result on scrap when possible.
Heat is a controllable variable, not a setting to choose once and ignore. For common 60/40 tin-lead solder on copper foil, a useful starting point is approximately 725 to 750 degrees F (385 to 399 degrees C). Many temperature-controlled irons work somewhere around 700 to 800 degrees F (370 to 425 degrees C), but the right setting depends on the iron, tip size, foil, panel, and movement speed. The iron setting is much hotter than the solder itself: common 60/40 tin-lead solder melts across an approximate 183 to 190 degrees C range, so the tip needs enough heat to transfer energy into the seam while you keep moving.
Begin near the lower-middle of the range on scrap or an inconspicuous seam. If the solder will not wet a clean, fluxed joint, check the tip and pace before raising the dial. If the bead runs too freely, the glass is exposed to prolonged heat, or foil starts lifting, reduce heat or move faster. Two irons showing the same number can deliver different results, so follow the equipment and solder manufacturer’s instructions and make one small change at a time. The guide to control soldering iron heat explains this balance, while the stained glass soldering iron guide covers tool selection.
Clean the tip periodically by wiping it on a water-wet sponge, then re-tin it with a small amount of solder. A bright, wetted tip should transfer heat smoothly. If your seam becomes chopped, lumpy, or reluctant to accept solder, stop and correct the tip condition before continuing. For a closer alloy comparison, compare stained glass solder alloys before committing to a full panel.
How Stained Glass Soldering Builds a Copper Foil Panel
In the copper foil method, the foil is more than an edge covering. It creates the metal surface that solder can bond to, allowing separate pieces of glass to become one panel. Careful preparation matters because a weak adhesive bond, dirty foil, or uneven heat can affect the seam before the solder bead is even started.
- Prepare and foil the glass. Clean each piece to remove grinder dust, cutting oil, and residue. Center copper foil on the edges, then burnish it firmly, especially at corners and seam edges. Choose a width that suits the glass and finished line. Press down any loose edge before assembly because heat can lift it.
- Assemble on a stable surface. Fit the foiled pieces together on a flat, heat-resistant surface and check alignment before applying heat. The support should prevent shifting or raised glass, helping solder flow across the joint instead of collecting on one side.
- Clean, then apply flux sparingly. Flux helps solder flow and bond to the copper foil, but more is not better. Use enough to wet the seam, not enough to puddle or spatter. Too much can contribute to pits and bubbles, while too little can leave irregular seams or exposed foil. For more detail on when and how to apply flux to copper foil, see the dedicated flux guide.
- Tack the panel before building the bead. Place a small amount of solder at intervals along the joints to hold the glass pieces in position. Work around the panel and check that the design remains aligned. Tack soldering is not the finished seam. It gives the panel enough stability for the continuous bead while leaving room to correct an alignment issue before fully covering the foil.
- Move the iron steadily along the seam. Feed solder to the heated foil and guide the iron at a controlled, continuous pace. The goal is a smooth bead that wets the foil without spilling across the glass. If the seam looks flat, slow slightly and add solder. If solder runs onto the glass, move more quickly. Wipe the iron tip periodically on a water-wet sponge so oxidation and residue do not interfere with heat transfer. A useful companion is this guide to control soldering iron heat.
- Finish the first face. Complete one side with a steady bead. Let the solder cool, inspect for gaps, and correct only obvious defects.
- Turn the panel and solder the reverse. Turn the panel only after the first side is solid and safe to handle. Flux and solder the reverse side with the same controlled movement, then let the work cool before further corrections. Soldering both faces strengthens the copper foil connection and balances the finished seam.
- Correct defects with one deliberate pass. Avoid repeatedly heating a small area because concentrated heat can stress glass or loosen foil. Let the panel cool, add only the necessary flux, and make one controlled correction. For the broader sequence from glass preparation through finishing, follow this copper foil panel construction guide.
How to Solder Lead Came Without Distorting the Joint
Lead came is an H-shaped channel that holds glass on each side. Soldered seams add strength, but heat must not collapse the channel or tear the soft metal. For profiles, assembly order, and panel structure, see this lead came panel assembly guide.
- Prepare the joint. Fit and support the came so the intersection cannot shift while you work. Remove dirt and visible oxidation with a suitable wire brush or other controlled cleaning method. A clean surface helps flux and solder wet the joint instead of rolling away. Work in good ventilation, wear eye protection, and keep hands away from the hot iron, molten solder, and heated panel.
- Practice before touching the panel. If lead came is new to you, cut a few short scraps and make test joints. This lets you learn how quickly the solder melts and how much pressure the came can tolerate. It is much easier to recognize a stable joint on scrap than to correct a distorted intersection in a finished panel.
- Apply flux sparingly. Brush a small amount over the cleaned seam rather than flooding the surrounding came. If solder rolls off, stop and inspect the joint. Insufficient flux, remaining dirt, or oxidation can prevent the solder from bonding. Clean and re-flux instead of repeatedly adding heat.
- Heat the solder and the came. Feed a small amount of solder to the joint and add more only as needed. Warm the solder and lead enough to form a union, but do not press the tip directly into the lead. Excess heat can deform the came, widen the channel, and change the glass alignment.
- Build the seam in small additions. A modest amount of solder is easier to control than a large puddle. Keep the iron moving as the solder flows across the intersection. Aim for a filled, connected seam, not a tall mound that makes inspection harder.
- Let the joint cool before turning the panel. Do not rotate, lift, or flip the panel immediately after the final seam. Molten solder and nearby came remain hot and mechanically vulnerable until they cool. Moving the panel too soon can pull the joint apart or introduce a twist that becomes difficult to correct.
- Finish with putty when the construction calls for it. Solder strengthens the came intersections, but it does not replace the glazing compound used to secure glass in the channels. Putty helps hold the glass and makes the joints watertight. Apply it only after the soldered structure has cooled and the panel is ready for that finishing stage.
Why Solder Beads Turn Lumpy, Flat, or Weak
Most solder defects have an observable cause. Before adding more metal, stop and inspect the seam, foil, flux, and iron tip. In stained glass soldering, a small change in heat, movement, or surface cleanliness can alter the entire bead.
Weak joints, exposed foil, and solder that rolls away
A cold or weak joint usually means the solder melted without properly heating the metal beneath it. Flux may be missing, spent, or applied to a dirty joint. Clean away residue and oxidation, apply a light, even coat of flux, and bring the iron and solder to the seam together. The goal is to heat the foil or came enough for the solder to bond, not simply to drop molten solder on top.
If solder rolls off instead of wetting the seam, check for insufficient flux or contamination first. Exposed foil and irregular coverage often point to too little flux, uneven foil contact, or moving before the solder has flowed across the copper. Recheck that the foil is firmly adhered and that the glass was cleaned before foiling. A stained glass soldering iron with a dirty tip can also transfer heat poorly, so wipe the tip periodically on a water-wet sponge. For more help diagnosing heat and movement, see this guide to control soldering iron heat.
Lumpy, chopped, or flat seams
A lumpy or chopped seam usually reflects inconsistent movement. Moving too quickly leaves unmelted solder; moving too slowly can let one area harden before the next joins it. Keep a steady pace and let the bead level before continuing. If the surface looks flat, slow slightly and add solder in controlled amounts rather than flooding the joint.
If solder spills onto the glass, the iron is likely traveling too slowly, the bead is oversized, or excess flux is making the molten solder move unpredictably. Increase your pace and reduce the amount added. Pits or bubbles commonly indicate too much flux or spatter. Let the seam cool, clean away residue, and rework only the affected area with a smaller amount of flux.
Repairing a mistake without stressing the glass
For an overbuilt section, place solder wick over the bead and heat the wick with the iron. The braided copper draws excess solder away, allowing you to reshape the seam. Work in short passes and avoid holding heat in one location. Repeated heating can stress or break glass, especially near a corner or narrow piece. Let the panel cool between repairs, then correct the remaining low spot with a small, deliberate addition of solder.
How to Finish and Clean a Stained Glass Solder Line
Let the panel and every soldered joint cool completely before you move, wash, or inspect it. Molten solder, dross, and recently soldered joints can cause burns until they have cooled. Turn off and unplug the iron, return it to its stand, and allow the equipment to cool fully before storing it. These precautions are especially important when a panel has many seams that retain heat.
When the work is cool, remove flux residue with a damp cloth. Do not use compressed air or dry wipes, which can spread contaminated particles. Wash your hands with soap and water, keep food and drinks away, and damp-wipe the work surface after soldering. Penn’s soldering safety guidance explains these cleanup practices.
Use the cleanup pass as a quality inspection. On copper foil seams, look for gaps, pinholes, exposed foil, or areas where solder did not bond. On a lead came panel, inspect each joint for oxidation, a white powdery appearance, or torn metal beside the soldered area. The National Park Service specifically identifies those conditions as signs to check when evaluating came. Do not hide a damaged joint with more solder. Stop, determine whether the joint needs careful rework, and avoid overheating the surrounding glass or came.
If your project uses leaded solder or lead came, collect solder drips, trimmings, and contaminated disposable materials rather than sweeping them into ordinary debris. Penn classifies leaded soldering waste as hazardous waste and recommends a lidded container. Follow your local disposal requirements. After the panel is clean and sound, patina can be considered as a later finishing choice. Treat it as a separate surface-finishing step, not a substitute for removing flux or correcting a weak seam.
Shop stained glass tools and soldering supplies
Frequently Asked Questions
What kind of solder do you use on stained glass?
For copper foil, 60/40 tin-lead solder is a common choice because it flows readily and supports a smooth bead. Some artists use 50/50 solder where a stiffer alloy is useful, especially for specific construction needs. Choose an alloy that suits the seam, follow its product instructions, and use the appropriate flux for copper foil or lead came.
Should you solder the front or back of stained glass first?
After tack soldering has stabilized a copper foil panel, complete one side before turning it over. Let the last joints cool fully, then support the panel as you work on the opposite side. This sequence reduces shifting and helps protect fresh seams. Do not rush the turn, since hot soldered joints can still deform or cause burns.
What is the Tiffany soldering technique?
The Tiffany technique is the copper foil method. Each glass piece is wrapped with adhesive-backed copper foil, then the foil-covered seams are fluxed and soldered together. Tack soldering first holds the arrangement in place, while a continuous solder bead reinforces and finishes the seams. This differs from lead came construction, where glass fits inside channels and the came joints are soldered.
What can I solder stained glass on?
Use a flat, stable, heat-resistant, noncombustible surface that supports the panel without trapping or stressing the glass. Keep the work area clear of food and drink, provide ventilation that draws smoke away from your breathing zone, and use a stand for the hot iron. Yale recommends local exhaust or bench-top extraction for soldering work, rather than relying on recirculating filtration alone: Yale safety guidelines.
Ready to Set Up Your Next Soldering Session?
Choosing the right iron, solder, flux, and safety supplies can make copper foil and lead came work easier to control. A well-matched setup also gives you more consistent seams and a cleaner finish as you practice different techniques.
Shop stained glass tools and soldering supplies
Browse the available supplies, then get started with the tools that fit your project and workspace.